TitanPro Cutting TitanPro Cutting

7 Best Ways to Avoid Common 5 Axis Toolpath Errors?

Time:2026-10-28 Author:Aria
0%

Five-axis machining promises shorter cycle times, fewer setups, and better access to complex surfaces. Yet greater freedom also creates more ways to fail. A small rotary-axis mistake can leave a visible witness mark, trigger a collision alarm, or damage an expensive tool. On the shop floor, these problems often appear after hours of simulation and preparation.

So, what are the common errors in 5 axis toolpath generation? Typical failures include gouging, tool-holder collisions, axis-limit violations, unstable tool orientation, abrupt rotary movements, and incorrect post-processor output. Poor linking moves can also leave uncut material between features. These errors become more serious when machines use different kinematic layouts, controllers, or rotary-axis conventions.

Industry research supports a careful approach. Deloitte’s 2024 Smart Manufacturing and Operations Survey found that 86% of manufacturers consider smart manufacturing important for competitiveness. However, digital capability does not remove basic programming risks. NIST research on smart manufacturing also emphasizes reliable data, verification, and interoperability across production systems. That lesson matters here. A perfect-looking simulation can still fail when machine geometry, fixtures, probing results, or post-processing settings differ.

This guide presents seven practical ways to reduce common five-axis toolpath errors. It focuses on verification, cutter selection, collision checking, tool-axis control, and disciplined machine testing. Some recommendations may feel obvious. They still get skipped. No checklist is perfect, and experienced programmers occasionally miss a single clearance value. The goal is not flawless software output. It is a safer, more repeatable process that catches expensive mistakes before metal is cut.
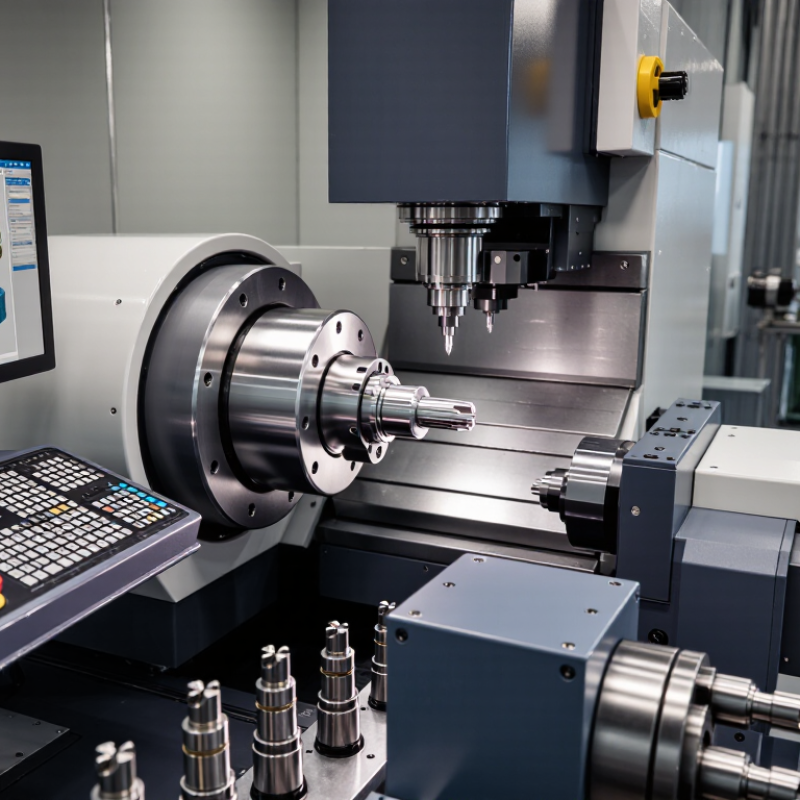
7 Best Ways to Avoid Common 5 Axis Toolpath Errors?

Define the Most Common 5-Axis Toolpath Errors

Five-axis toolpath errors are rarely dramatic at the start. They often appear as small angular changes, unexpected marks, or unstable cutting.

A common error is tool-axis singularity, where rotary axes approach an awkward alignment. The machine may suddenly rotate, pause, or choose a longer motion. The danger is subtle. Another frequent problem is gouging. The cutter contacts a surface that the simulation did not properly protect, especially near deep pockets, thin walls, or sharp transitions.

Poor lead and lag angles create uneven cutting pressure. The tool may rub instead of cut, leaving cloudy surfaces or heat discoloration.

Excessive axis movement can also produce visible witness marks. This usually happens when the toolpath changes orientation too often.

Chordal error is another concern. If the programmed points are too widely spaced, the cutter follows a rough approximation of the intended surface. That mark matters.

In practical inspections, I check the setup, tool length, work offset, and post-processed code together. A correct model cannot rescue incorrect machine data. Collision errors may involve the holder, spindle nose, fixture, or an unmodeled clamp. I once treated a minor fixture contact as a simulation issue, but the real cause was incomplete setup geometry. That mistake was avoidable. Reliable verification compares machine limits, tool access, surface tolerance, and actual rotary behavior. Cutting tests should use a manageable feed rate and a visible inspection area. Even experienced programmers should question sudden axis reversals, because a smooth simulation can still hide an unsuitable machine motion.

Verify Machine Kinematics and Coordinate Settings

5 Axis Toolpath Verification: Machine Kinematics and Coordinate Settings

Reliable five-axis machining begins with accurate machine kinematics. The CAM simulation must match the machine’s rotary axes, travel limits, pivot location, and rotation direction. A small mismatch can move the tool several millimeters near a tilted workpiece.

I once trusted a simulated toolpath without checking the rotary zero position. That assumption was wrong. The machine rotated around a different reference point, causing an unexpected tool approach. Now, I compare the digital machine model with the actual setup sheet. I verify axis labels, rotary centers, TCP settings, and work offset values before posting code. I also confirm whether the controller uses tool-center-point compensation during simultaneous motion.

Coordinate settings need equal attention. The part origin, fixture location, and machine datum should agree across CAD, CAM, and the control. A misplaced origin may produce correct-looking motion in simulation but unsafe contact at the machine. Test the code above the workpiece first. Use a reduced feed rate and observe rotary movement carefully. Do not rely on visual confidence alone.

Tips: Record the actual rotary zero positions. Check the post processor after any machine configuration change. Run a dry cycle with the tool clear of clamps and the stock. Measure the first setup, even when the simulation looks perfect. Small errors grow quickly. My own checks are still evolving, because every machine reveals different assumptions.

7 Best Ways to Avoid Common 5-Axis Toolpath Errors

Verify Machine Kinematics and Coordinate Settings

The chart shows the theoretical tool-center-point displacement caused by a single rotary-axis angular error at a 250 mm pivot radius. The values are calculated using displacement = 250 × tan(angle), demonstrating why small kinematic calibration errors can create visible gouging, dimensional variation, or incorrect tool orientation.

  • Verify rotary-axis zero positions and machine kinematic parameters.
  • Confirm the active work coordinate system before loading the toolpath.
  • Check tool length, radius, and pivot-point compensation values.
  • Use the correct post-processor for the machine configuration.
  • Simulate rotary-axis motion and inspect tool-center-point behavior.
  • Run a controlled dry cycle above the workpiece.
  • Measure the first test cut and update offsets only after confirming the cause.

Calculation basis: single-axis angular error at a 250 mm radius; results exclude additional machine geometry, thermal, fixturing, and tool deflection errors.

Optimize Tool Orientation and Collision Avoidance

7 Best Ways to Avoid Common 5 Axis Toolpath Errors

Optimize Tool Orientation and Collision Avoidance In five-axis machining, tool orientation controls both surface quality and collision risk. Experienced programmers inspect the holder, spindle nose, fixtures, and cutting tool length before generating paths. A short tool is usually more stable. However, it may not reach deep features. Set lead and tilt angles carefully, then check their effect across every surface.

Use collision simulation with accurate machine geometry, stock, clamps, and fixtures. Do not trust color maps alone. They can hide small clearance problems near corners. Define safe zones around the workholding system, and limit rotary-axis motion near singularities. Smooth orientation changes reduce sudden movements and visible marks. Abrupt changes often indicate poor point distribution or an unsuitable cutting direction.

A practical workflow compares several tool orientations before finalizing the path. I once accepted a clean simulation, but the real setup revealed a tight holder clearance. The model was incomplete. That mistake changed my checking routine. Now, I review the most difficult areas manually and run a cautious dry cycle. Leave extra clearance where possible, even when it reduces cutting efficiency. It is not always the fastest choice. Check retracts, rotary limits, and approach moves separately. Small errors often appear there, not during the main cut.

Control Cutting Parameters and Toolpath Smoothing

5 Axis Toolpath Errors: Control Cutting Parameters and Toolpath Smoothing

Five-axis errors often begin with unstable cutting parameters, not the machine itself. Excessive radial engagement can overload a small cutter during sharp rotary moves. Excessive feed can leave visible scallops on steep surfaces. A 2023 U.S. Department of Energy manufacturing assessment report noted that process optimization can deliver measurable energy savings, often above 10% in assessed plants. That matters because unstable cutting also wastes power, inserts, and inspection time.

Use a controlled feed strategy. Reduce feed during tight tool-axis changes, then restore it on open passes. Keep the feed per tooth consistent when spindle speed changes. Check chip load at the actual contact point, not only in the CAM table. Toolpath smoothing should remove tiny directional commands without flattening important geometry. Excessive smoothing can create dimensional drift near holes, edges, and thin walls. I have seen a clean simulation produce chatter because the real fixture flexed slightly. Simulation is useful, but it is not proof.

Tips: Start with a conservative step-over and a 10–15% lower feed near axis reversals. Review machine-code blocks for short segments. Compare spindle load, sound, and surface finish after each adjustment. The ISO 230-1 standard stresses machine-tool accuracy testing, yet cutting behavior still depends on setup rigidity and tool condition. That is where many “perfect” toolpaths fail. Record the correction, but question it later.

Simulate, Inspect, and Safely Validate the Final Toolpath

A reliable five-axis toolpath begins with a complete model check. Remove tiny faces, open surfaces, and unclear edge transitions before programming. I inspect the stock definition against the actual billet on the machine. Wrong stock dimensions can hide a collision. That mistake is common.

Simulation comes next. I run the entire path, not only the difficult corners. I watch tool-axis changes near deep pockets, thin walls, and clamps. Slow playback reveals sudden rotary movement and unsafe retracts. I also check remaining material with a comparison view. A clean animation is not proof of safety. The simulated holder, fixture, and machine limits must match reality.

Inspection should include gouge detection, flute engagement, feed changes, and minimum clearance. I measure the tightest gap numerically instead of trusting screen color. Then I review the code line by line around rapid moves and rotary-axis reversals. A second programmer should challenge the setup. Fresh eyes find assumptions I miss. I once approved a path after checking the cutter but forgetting the collet. The simulation looked perfect, yet the clearance was marginal. Now I validate the complete assembly, verify work offsets, and test the first run at reduced speed. I keep the operator beside the control and stop immediately when motion differs from the simulation. Seven habits help: clean geometry, accurate stock, full simulation, collision checks, clearance measurement, code inspection, and controlled prove-out. None replaces judgment.

FAQS

Why must machine kinematics match the five-axis simulation?

Rotary axes, travel limits, pivot locations, and rotation directions must agree. A small mismatch can shift the tool several millimeters near a tilted workpiece. I once trusted the simulation too quickly.

Which machine settings should be checked before posting code?

Compare the digital machine model with the actual setup sheet. Check axis labels, rotary centers, TCP settings, and work offsets. Confirm how the controller handles tool-center-point compensation.

How can coordinate errors create unsafe motion?

The part origin, fixture location, and machine datum must agree. A misplaced origin may look correct in simulation but contact the workpiece. Small coordinate errors grow quickly.

What should operators do during the first machine test?

Test the code above the workpiece with the tool clear of clamps. Use reduced feed and watch rotary movement carefully. Stop immediately if the motion differs.

Why is accurate stock modeling important?

The simulated stock should match the actual billet dimensions. Incorrect stock can hide collisions or leave unexpected material. This mistake is common.

What areas deserve close attention during full simulation?

Watch deep pockets, thin walls, clamps, retracts, and sudden tool-axis changes. Run the entire toolpath, not only difficult corners. Slow playback helps.

What safety checks should a final toolpath include?

Check gouges, flute engagement, feed changes, minimum clearance, and remaining material. Measure the narrowest gap numerically. Screen colors are not enough.

Why should another programmer review the setup?

A second person can question hidden assumptions and missed clearances. Review the code around rapid moves and rotary reversals. Fresh eyes help.

Conclusion

Avoiding common 5-axis toolpath errors begins with understanding how they occur, including incorrect tool orientation, unexpected collisions, excessive rotary-axis movement, gouging, overcutting, and poor surface quality. A reliable workflow starts by verifying the machine’s kinematics, coordinate systems, work offsets, rotary-axis limits, and post-processing settings. These checks help ensure that the programmed motion matches the actual machine configuration and prevents errors caused by mismatched settings. When asking “what are the common errors in 5 axis toolpath generation,” it is important to consider both programming and machine-related factors.

Tool orientation should be optimized to maintain stable cutting conditions and adequate clearance from the workpiece, fixtures, and machine components. Cutting speed, feed rate, step-over, and smoothing settings should also be balanced to reduce vibration and sudden axis changes. Finally, the completed toolpath should be simulated, inspected, and safely validated through careful verification of material removal, collision risks, axis travel, and machine limits. This structured process improves accuracy, surface finish, machining efficiency, and overall production safety.
Aria

Aria

Aria is a dedicated marketing professional with a deep passion for innovative strategies and a keen understanding of our company's product offerings. With a wealth of experience in the industry, Aria excels at crafting engaging content that highlights the unique features and benefits of our......